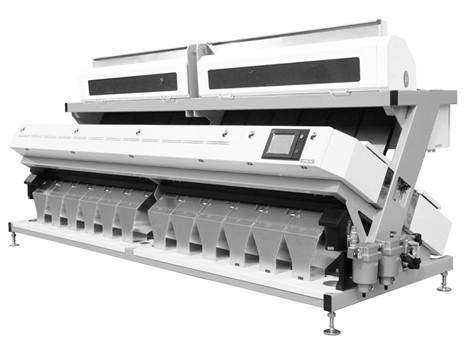
Lentils Color Sorter: Optimizing Quality and Efficiency in Lentil Processing
Introduction to Lentils Color Sorter
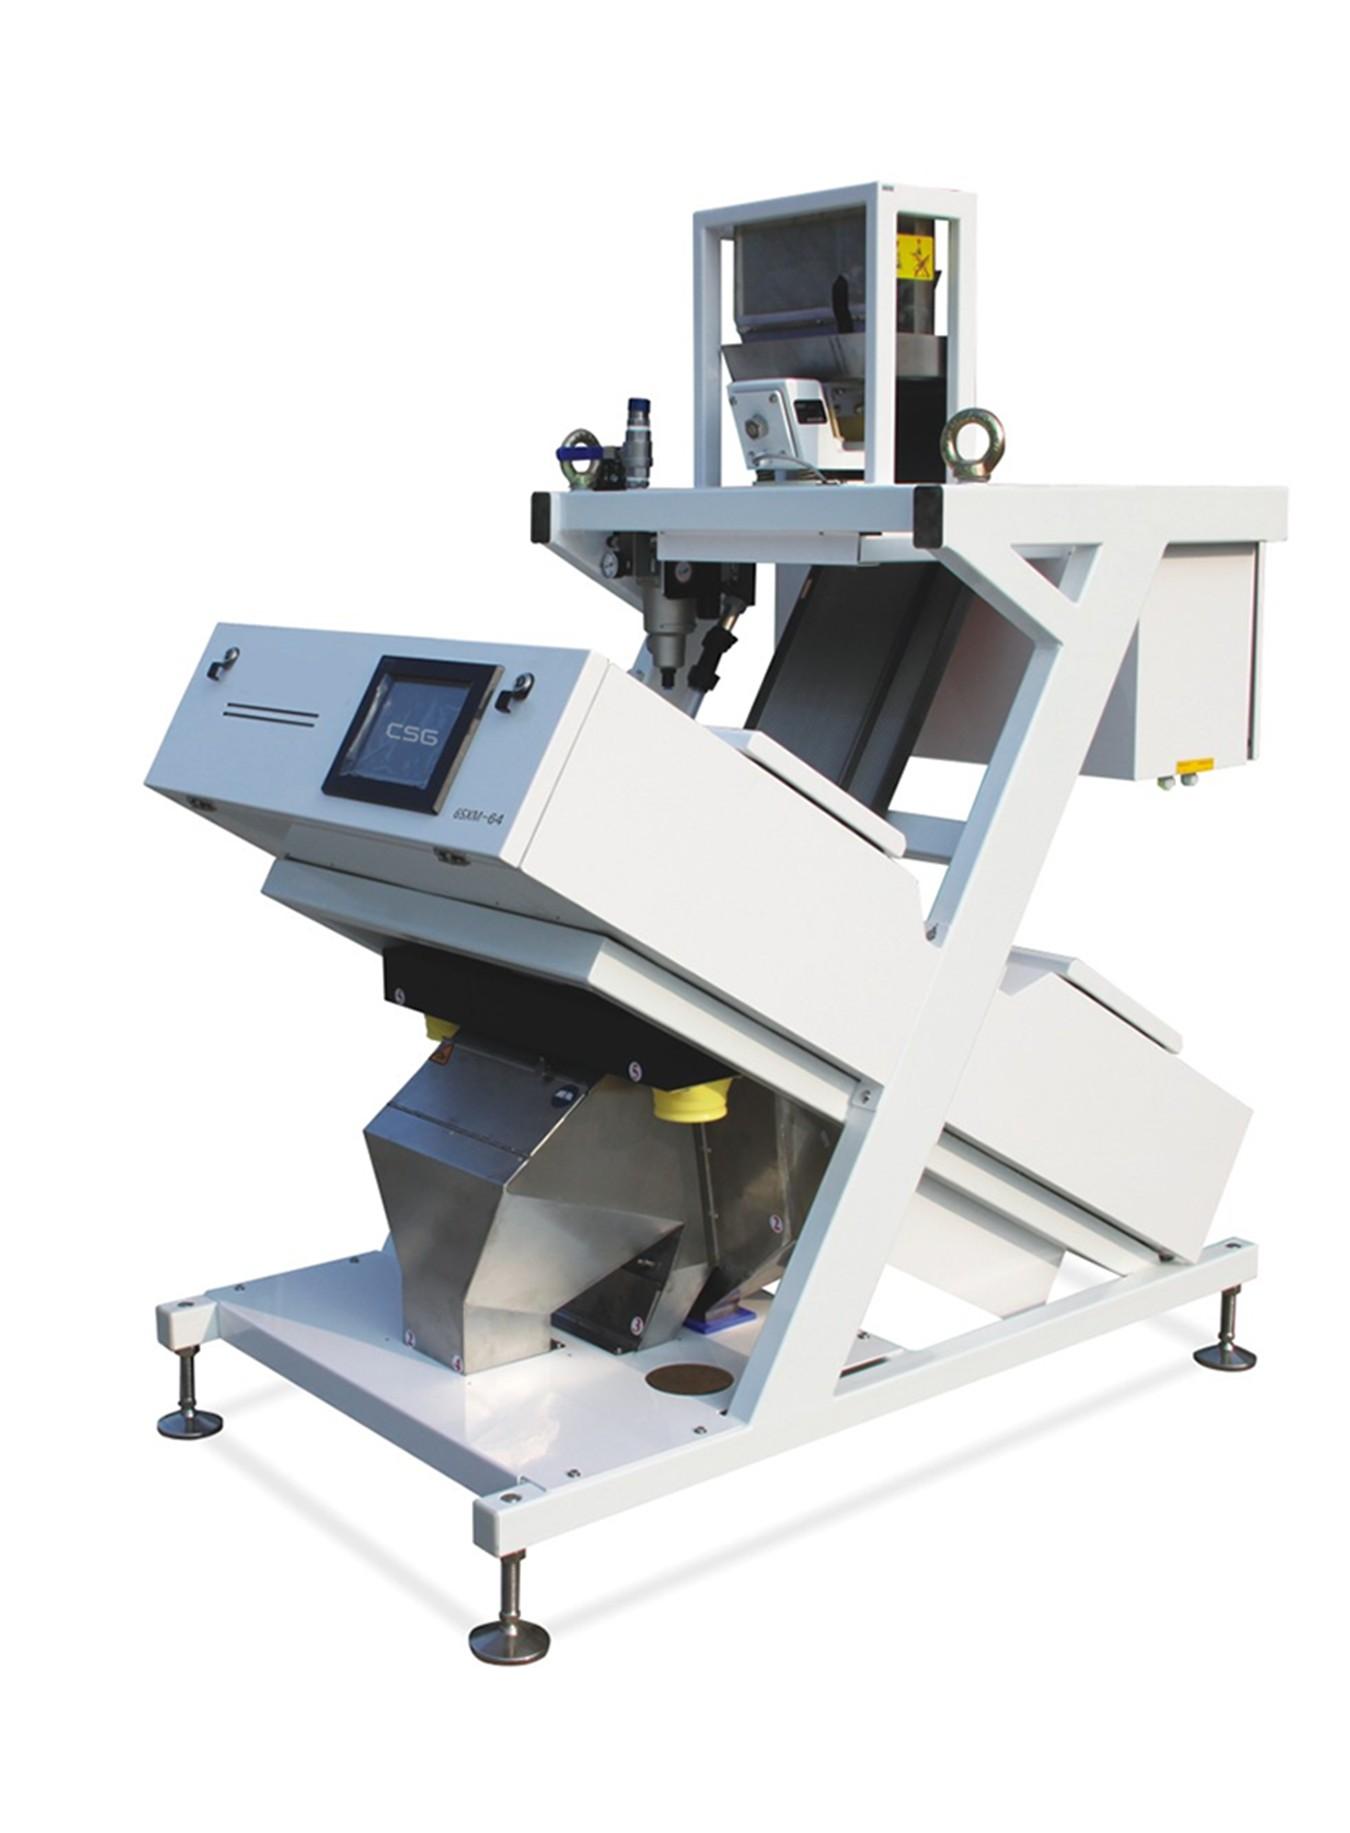
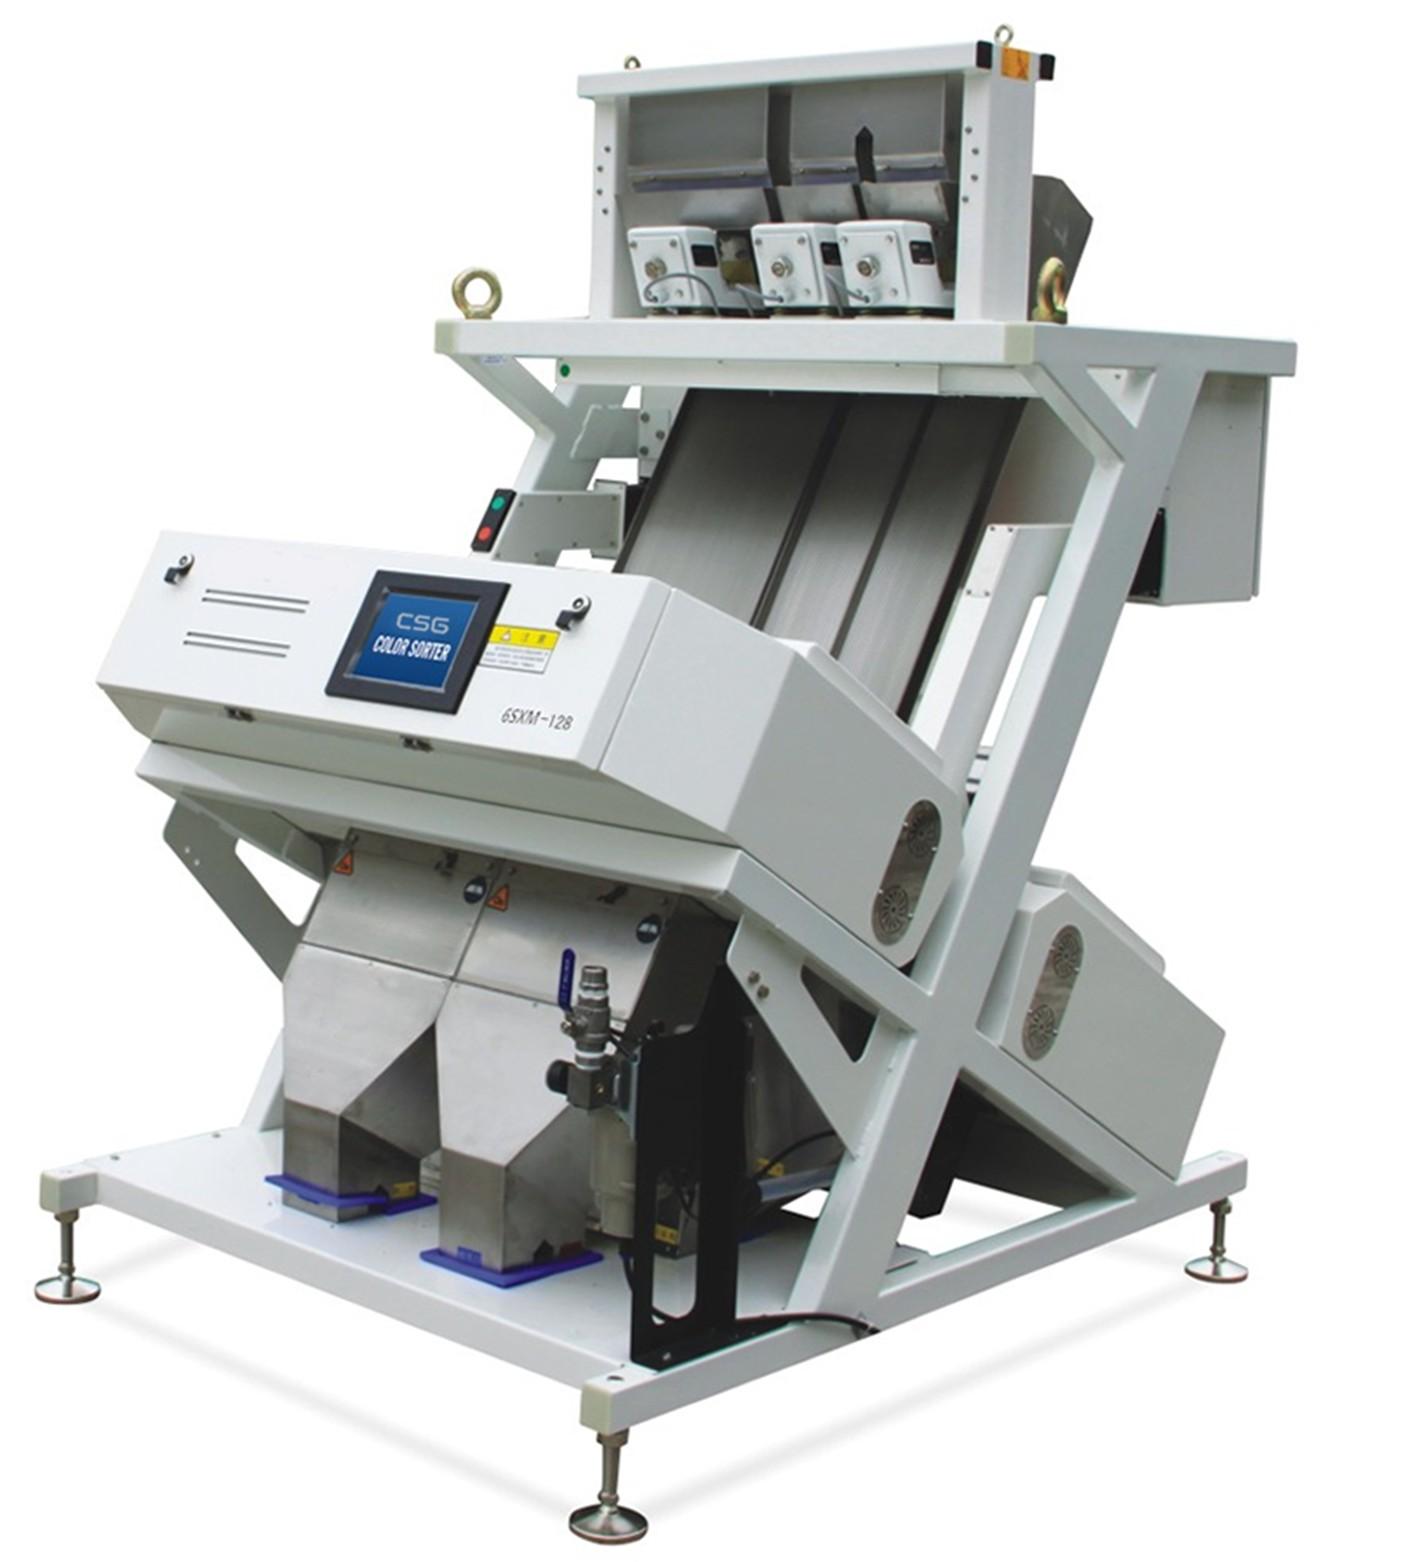
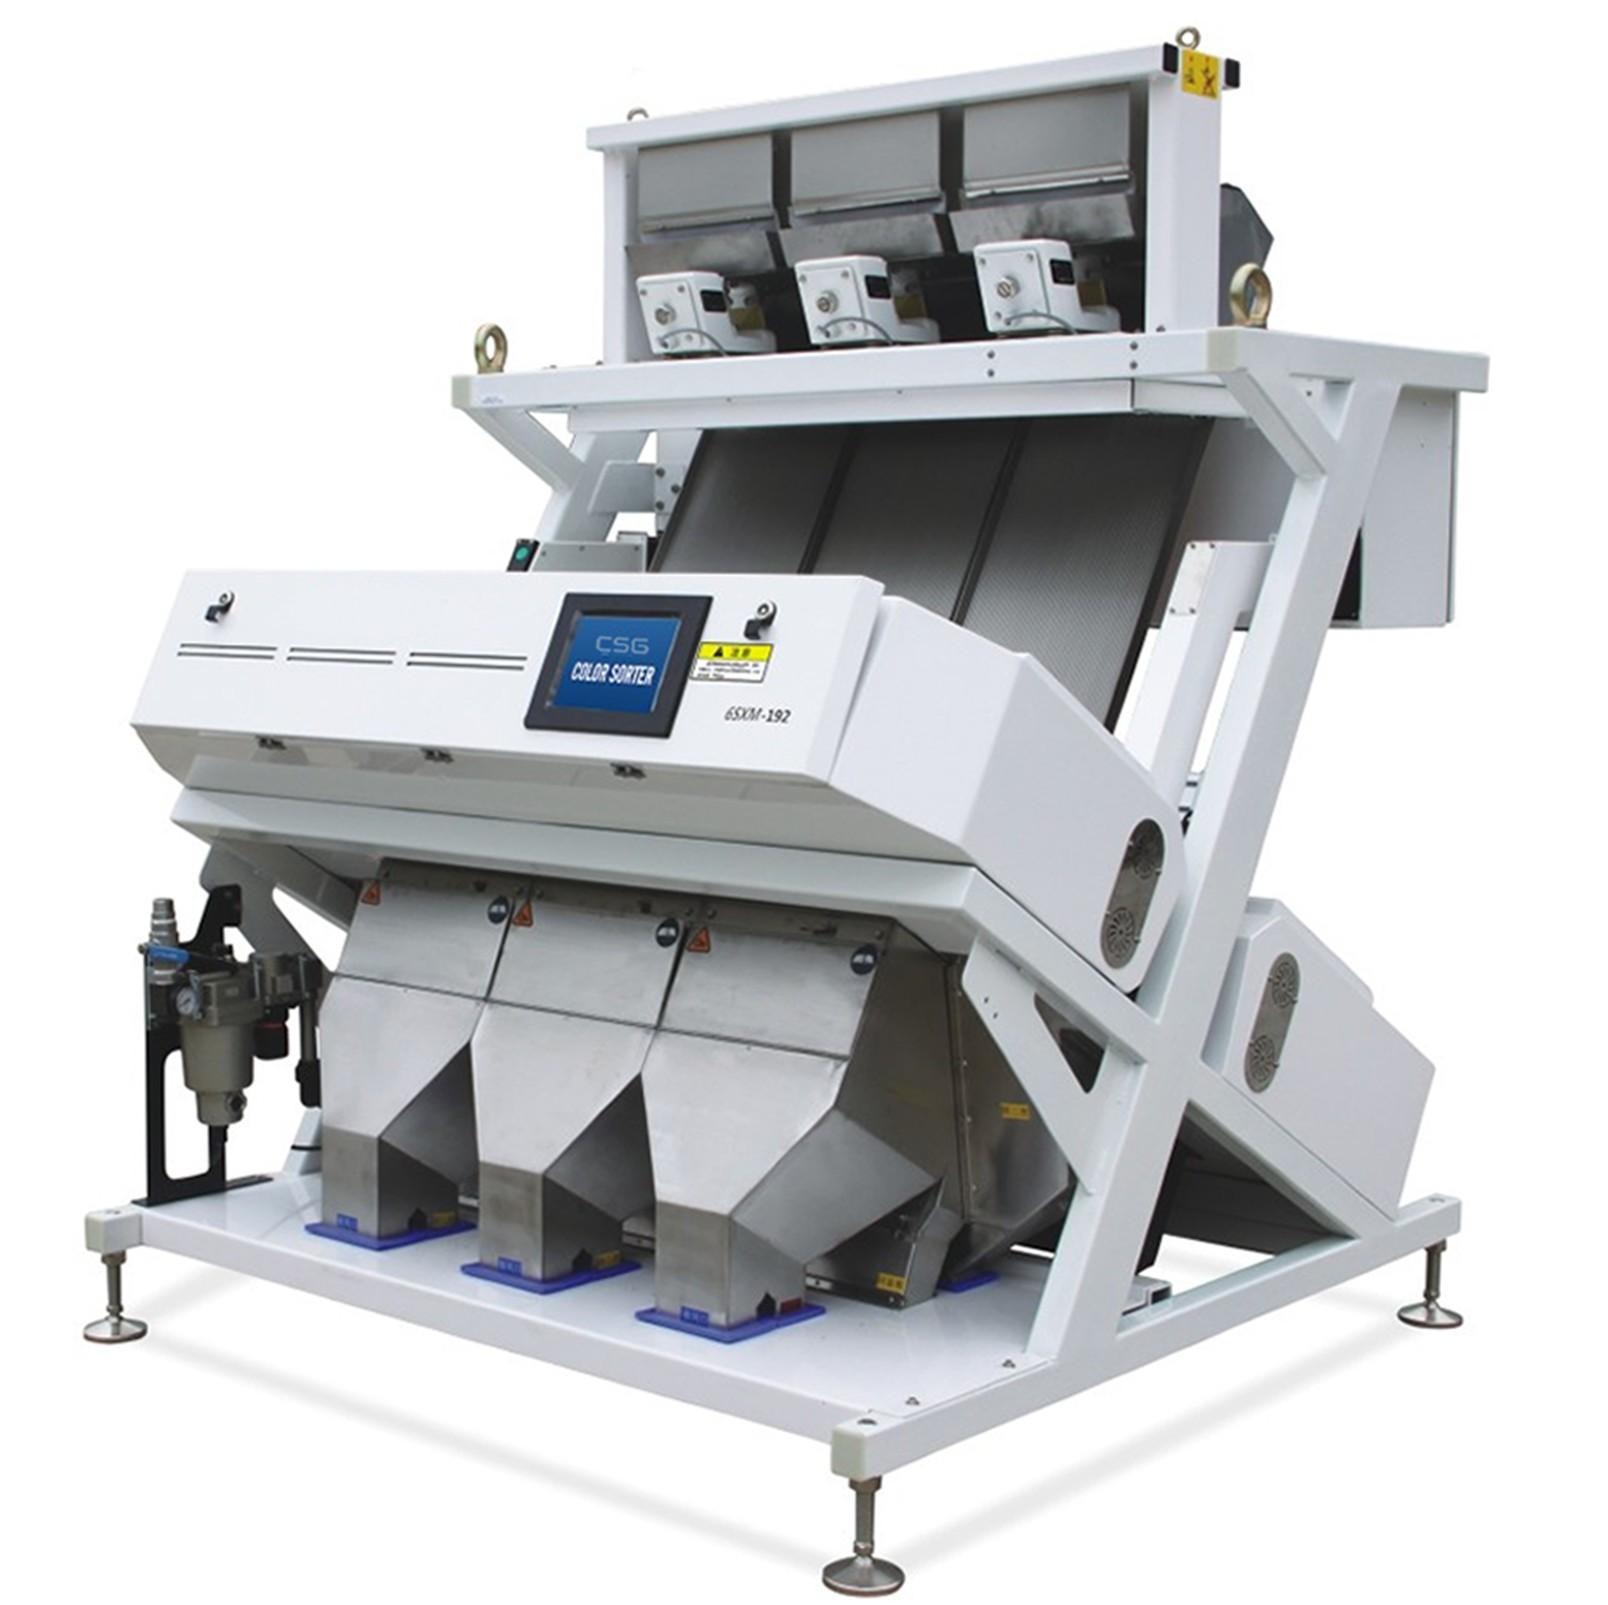
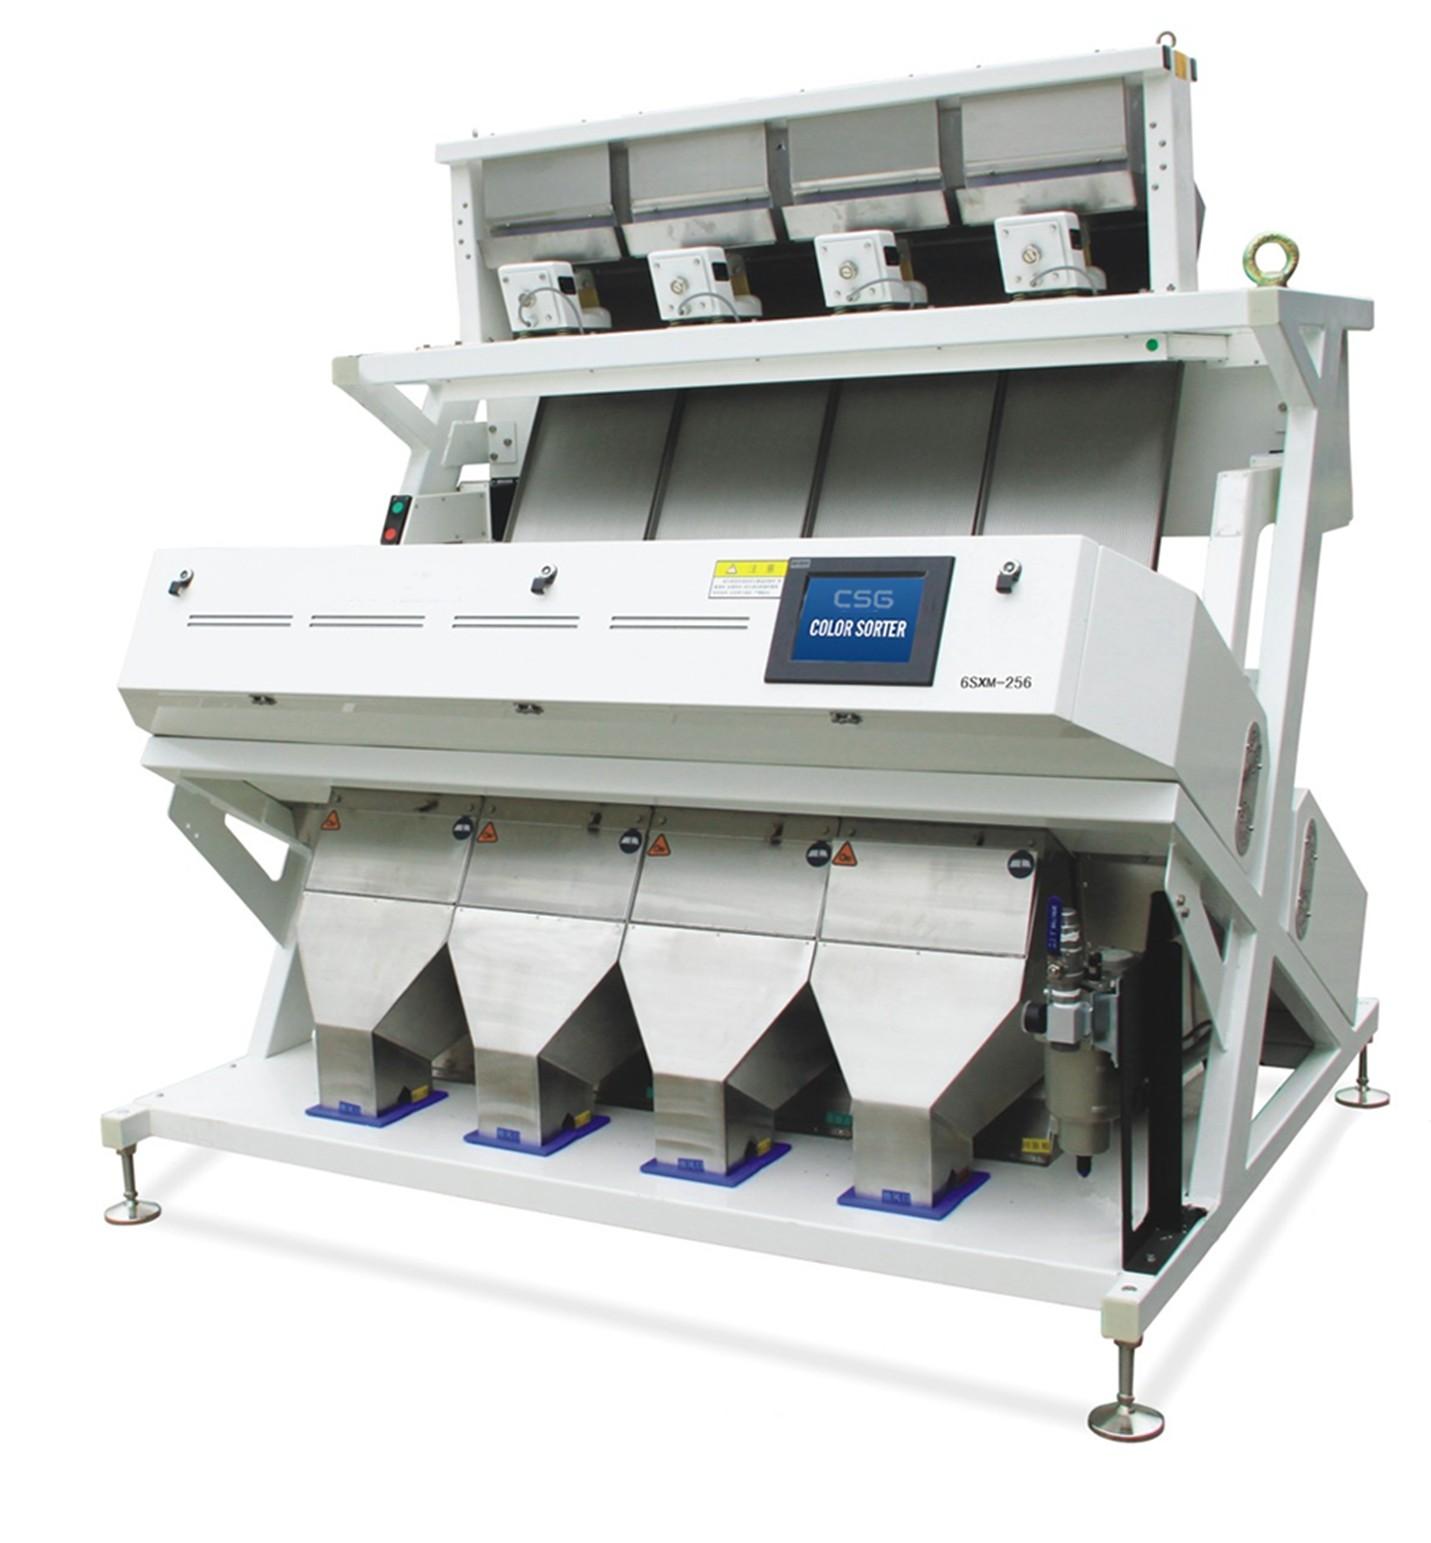
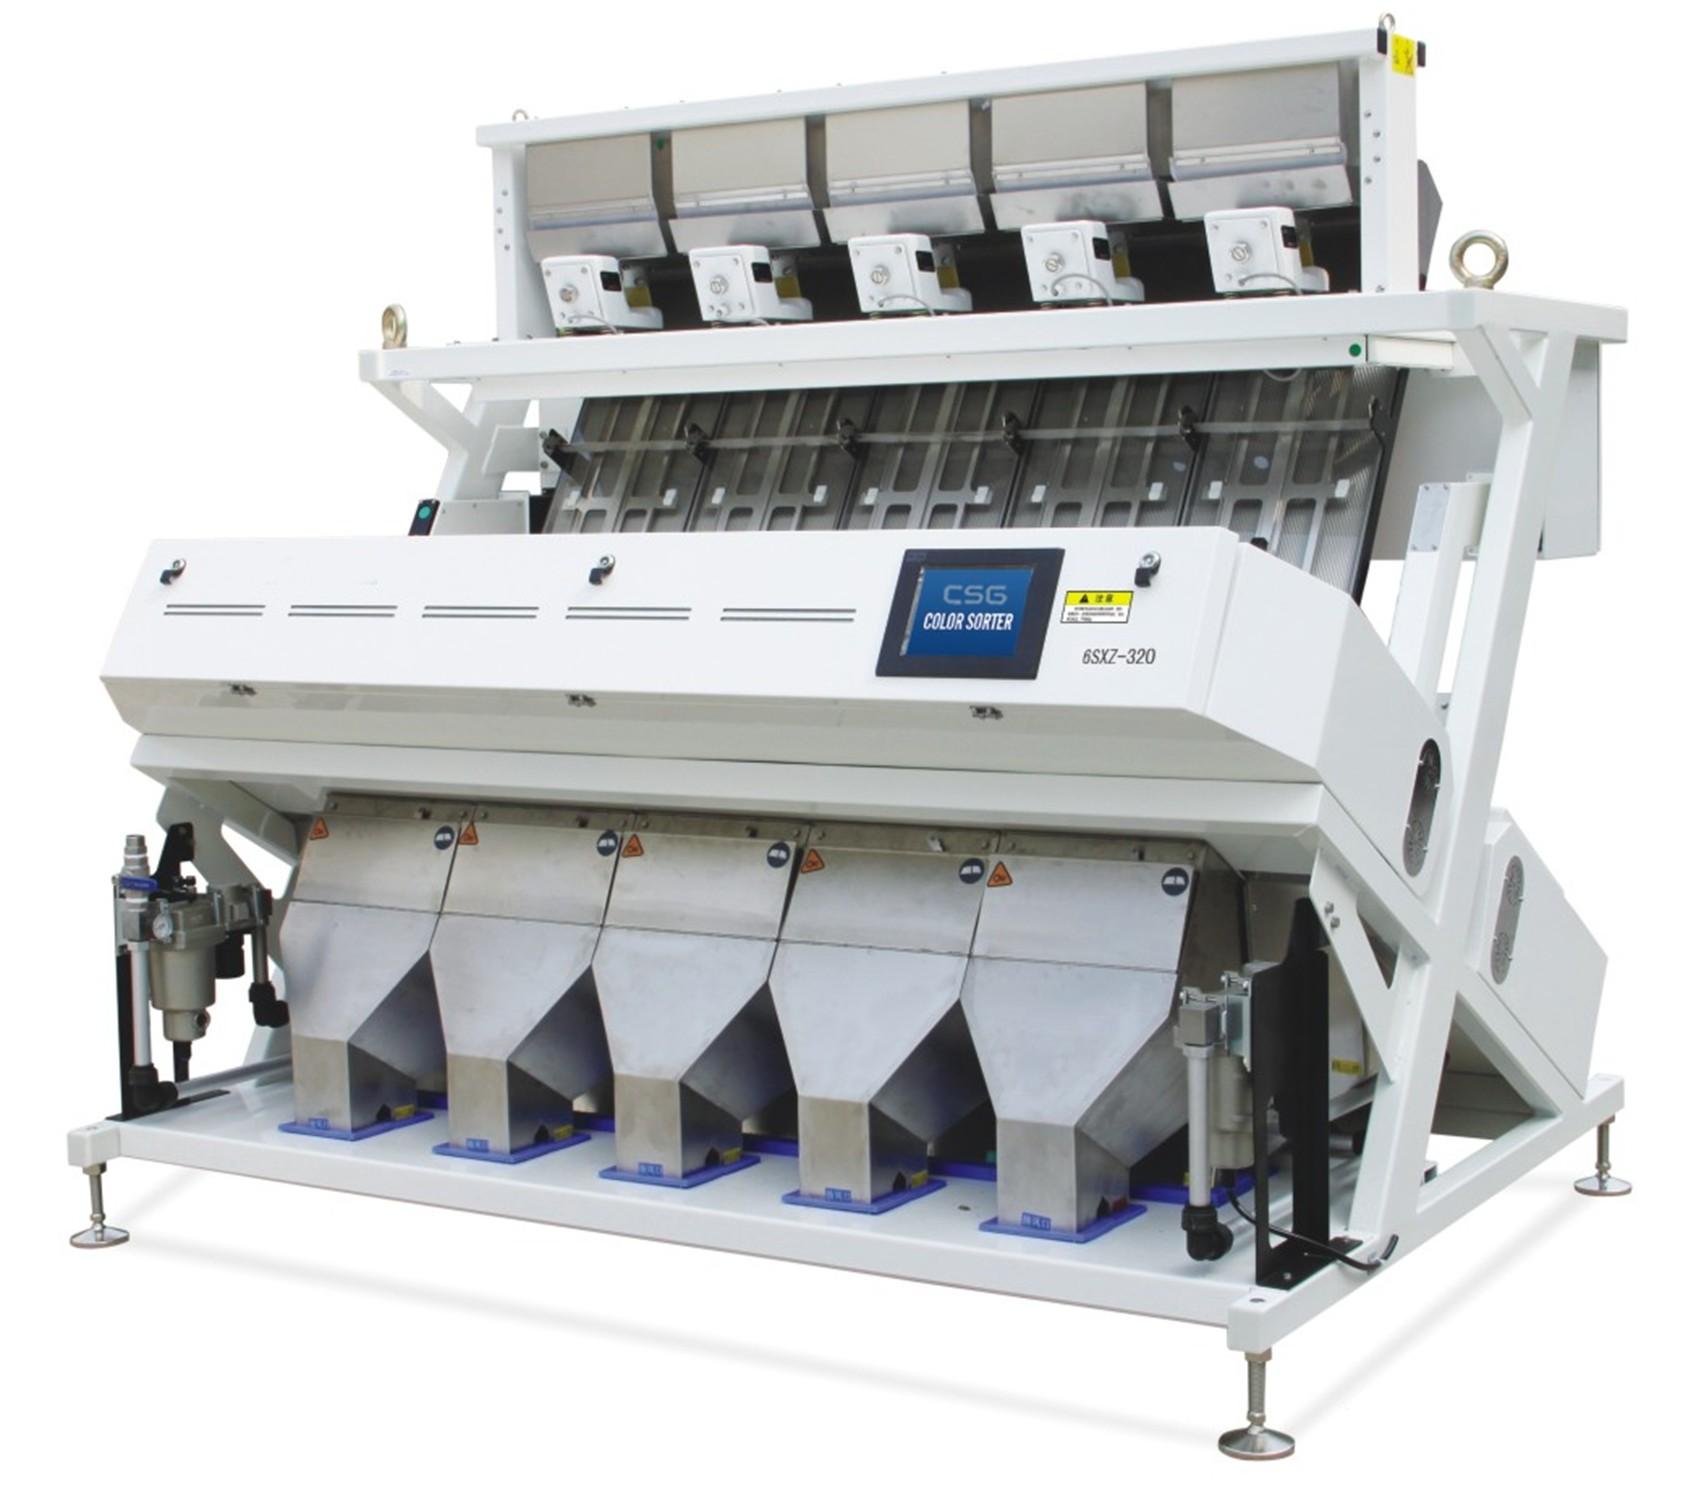
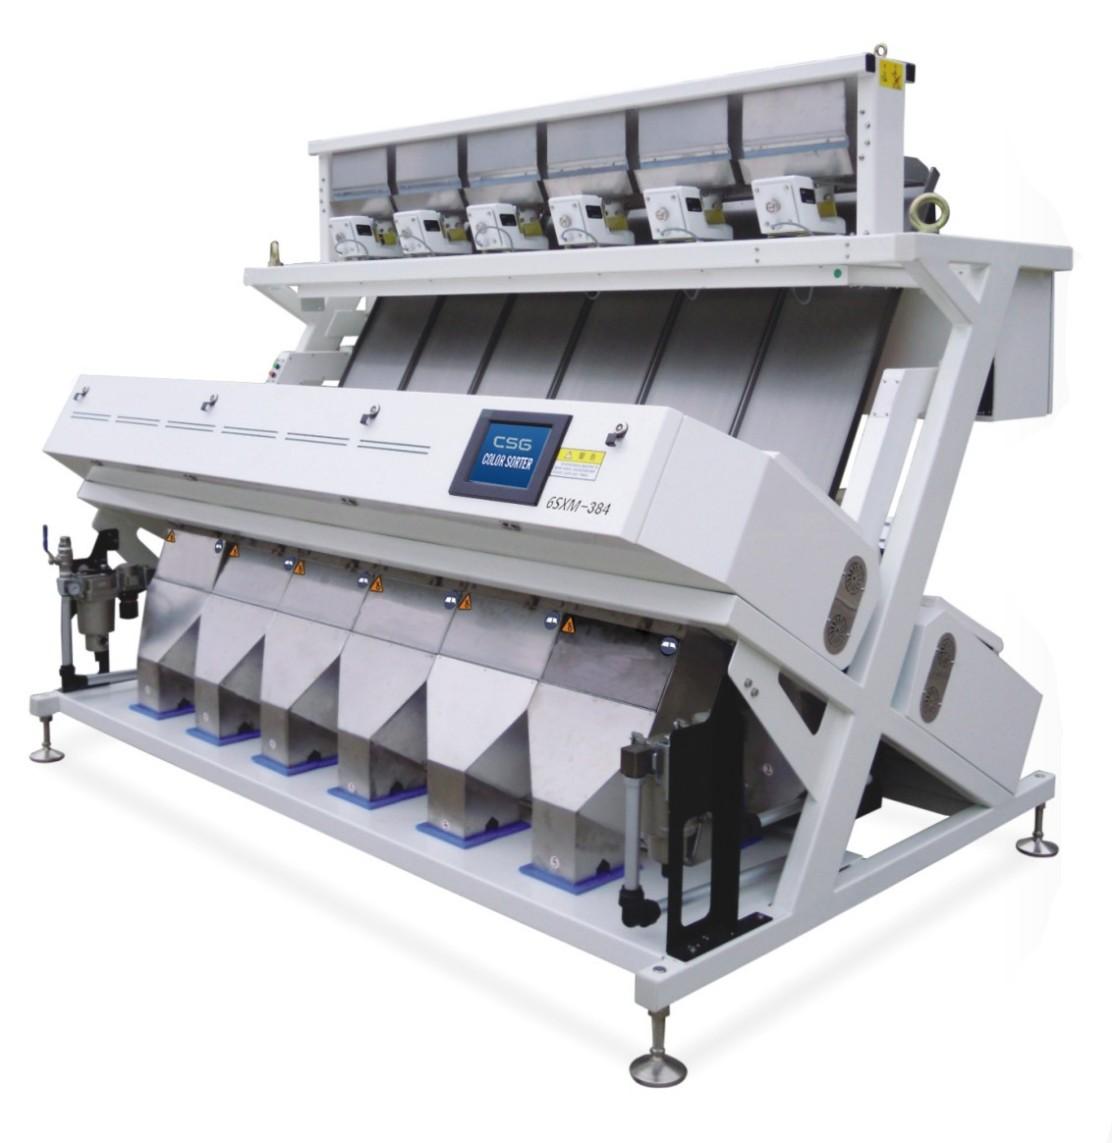
A lentils color sorter is a state-of-the-art optical inspection machine designed to enhance the quality and efficiency of lentil processing. It utilizes advanced multispectral imaging technology combined with intelligent recognition algorithms to sort lentils based on subtle color variations, effectively removing impurities, foreign seeds, stones, discolored grains, and defective lentils that compromise product quality and market value.
By incorporating a lentils color sorter into the processing line, lentil producers can significantly improve the overall quality of their products while reducing waste and increasing efficiency. The technology has become indispensable for processors seeking to meet the exacting visual quality standards of international export markets, domestic retail channels, and food manufacturing customers worldwide.
How Does It Work?
Lentils color sorters employ high-resolution CCD or CMOS cameras and sophisticated image processing algorithms to detect subtle color differences in lentils at high production speeds. As the lentils pass through the machine in a controlled single-layer flow, multiple cameras capture detailed images of each individual grain from different viewing angles. The onboard processing system analyzes these images in real-time, comparing each lentil against pre-configured acceptance criteria to identify discolored, mold-affected, insect-damaged, or otherwise defective grains as well as foreign materials.
Once a defective lentil or foreign particle is identified, the sorter utilizes high-speed pneumatic ejection mechanisms to remove the unwanted material with millisecond precision. This targeted removal ensures that only high-quality lentils proceed further in the processing line while maintaining maximum throughput and minimizing the loss of acceptable product.
Lentil Defect Detection by Variety
| Lentil Variety | Common Defects & Foreign Materials | Min. Defect Size | Detection Rate | Recommended Sensor Setup | Key Sorting Challenge | Typical Throughput |
|---|---|---|---|---|---|---|
| 🟤 Red Lentils (Masoor) | Discolored brown grains · Black seeds · Foreign pulses · Stones · Soil clods · Insect-damaged grains · Mold spots · Split lentils | ≥ 0.1 mm | ≥ 99.5% | RGB + NIR · Dual-side cameras · Multi-angle illumination | Natural color variation in red lentils · Small seed size inspection · High-volume processing for split lentil market | 2-8 t/h |
| 🟢 Green Lentils | Yellowed grains · Brown discoloration · Foreign seeds · Stones · Bleached spots · Insect holes · Weather damage · Soil particles | ≥ 0.1 mm | ≥ 99.4% | RGB + NIR · Multi-spectral · High-contrast green detection | Subtle yellowing detection · Green color uniformity for premium markets · Bleached vs. natural pale differentiation | 2-7 t/h |
| 🟡 Yellow Lentils (Toor/Pigeon Pea) | Dark spots · Discolored grains · Foreign pulses · Stones · Mold-affected grains · Insect damage · Shriveled seeds | ≥ 0.12 mm | ≥ 99.3% | RGB + NIR · Multi-angle cameras · Bright-field illumination | Dark spot detection on yellow surface · Split vs. whole grain differentiation · Consistent color for dal quality | 2-8 t/h |
| 🟤 Brown Lentils & Others | Black seeds · Foreign grains · Stones · Soil · Ergot · Mold · Insect damage · Shriveled grains · Split pieces | ≥ 0.15 mm | ≥ 99.2% | RGB + NIR · Enhanced foreign material detection · Shape analysis | Dark product subtle defect detection · Foreign seed identification · Soil clod vs. lentil differentiation | 1-6 t/h |
Benefits of Using a Lentils Color Sorter
By removing defective lentils and impurities, lentils color sorters ensure a higher quality end product, meeting stringent quality standards for premium export and retail markets worldwide.
Automating the sorting process significantly enhances processing speed and efficiency, leading to higher throughput and reduced processing time compared to manual hand-sorting labor.
Minimizing the presence of defective lentils reduces waste and maximizes yield, resulting in significant cost savings for lentil producers across every processing season.
By eliminating impurities, foreign materials, and mold-affected grains, lentils color sorters contribute to the overall safety and hygiene of the final lentil products.
Lentil Quality Grade Classification
| Grade | Designation | Max Defect Rate | Visual Quality Characteristics | Typical Market Application | Price Position | Industry Standards |
|---|---|---|---|---|---|---|
| A | Premium Export Grade | ≤ 0.5% | Uniform variety-specific color · Zero foreign seeds or grains · No stones or soil · No mold or insect damage · Plump uniform size · Bright clean appearance | Premium retail packaging · International export · High-end food service · Specialty dal products · Organic certification markets | Top Tier +20-35% | USDA No. 1 · EU Class I · Codex Stan 171 |
| B | Standard Commercial Grade | ≤ 2.0% | Generally uniform color · Minor variation acceptable · Trace foreign material within limit · Sound wholesome grains · Acceptable moisture content | Supermarket retail · Food service supply · Dal milling · Ingredient manufacturing · Domestic wholesale | Standard Market Price | USDA No. 2 · BRC Food · IFS Food · National Standards |
| C | Processing / Feed Grade | ≤ 5.0% | Mixed color acceptable · Variable grain sizes · Foreign material must be removed · Higher defect tolerance · Acceptable for further processing | Lentil flour milling · Protein extraction · Animal feed · Pet food ingredients · Industrial processing | Economy -15-25% | USDA Substandard · Feed Safety Standards |
Applications
Lentils color sorters find applications across various stages of lentil processing, from initial post-harvest cleaning through to final pre-packaging quality verification. The versatility of modern optical sorting platforms allows processors to handle multiple lentil varieties with simple recipe changes.
They are essential equipment in lentil processing facilities, ensuring the production of high-quality lentil products for consumers worldwide. From small-scale organic producers to multinational pulse trading companies, optical sorting technology provides the consistent, verifiable quality assurance that modern lentil supply chains demand.
Conclusion
Lentils color sorters play a vital role in modern lentil processing, offering a range of benefits from improved quality and efficiency to waste reduction and enhanced food safety. By investing in this advanced technology, lentil producers can elevate their production standards and meet the demands of discerning consumers in the global market. As international quality standards for pulses continue to tighten and consumer expectations for visual quality and purity increase, optical sorting technology will remain an essential competitive advantage for forward-thinking lentil processing operations worldwide.
Articles about Lentil Sorting
How to Choose the Right Channel Number for Your Lentil Color Sorter Based on Processing Capacity
A comprehensive guide to selecting the right channel number for your lentil color sorter. Learn how to match processing capacity with machine configuration, calculate throughput requirements, and...